

 English
 Français
 Português

 Home / Author / Chen Yuhan, After-sales Coordinator (OEM/ODM Silicone Products) / Polyether-Modified Silicone Oil: Structure, Performance, Applications, and Manufacturing Excellence
Polyether-Modified Silicone Oil: Structure, Performance, Applications, and Manufacturing Excellence
2026-09-21
Polyether-modified silicone oil is a high-performance organosilicon material developed for formulations that require rapid wetting, efficient spreading, stable dispersion, and broad compatibility. By combining hydrophobic siloxane segments with hydrophilic polyether segments, this functional silicone material addresses several limitations associated with conventional silicone oils and ordinary surfactants. It can improve the interaction between water, polar solvents, non-polar solvents, solid surfaces, coatings, fibers, plant leaves, polymers, and other formulation components.
The material is especially valuable where low surface tension and formulation stability must be achieved at the same time. Conventional silicone oils may offer excellent spreading but can show limited compatibility with water-based systems. Traditional surfactants may provide water compatibility but lack the same degree of spreading, surface activity, temperature resistance, and durability. Polyether-modified silicone oil balances these properties through carefully designed molecular architecture.
Product model LD-810 is a representative polyether-modified silicone oil supplied for use in agriculture, textiles, coatings, inks, daily chemicals, plastics, polyurethane, and other industrial applications. The product is identified by CAS No. 68937-55-3, EINECS No. 614-823-3, and a stated purity of 99.8%. It is also commonly described as a polyether silicone surfactant.
The following article explains the product’s structural characteristics, technical advantages, application performance, formulation considerations, quality controls, and the manufacturing strengths supporting stable supply. It also discusses why an experienced silicone-material producer and supplier is important when customers require customized performance rather than a generic additive.
Polyether-Modified Silicone Oil
1. Product Overview
Polyether-modified silicone oil is formed by introducing polyether chains into the backbone or side-chain structure of silicone oil. The resulting molecule contains both silicone-based and polyether-based functional regions. The siloxane portion contributes low surface energy, flexibility, spreading ability, lubrication, and resistance to temperature and aging. The polyether portion provides polarity, hydrophilicity, water compatibility, and improved interaction with polar materials.
This amphiphilic molecular structure enables the material to position itself at interfaces. In a water-based formulation, the polyether segments interact with the aqueous phase while the siloxane segments orient toward hydrophobic surfaces or air interfaces. This interfacial arrangement can lower surface tension and improve contact between a liquid and a solid. The effect is useful in agricultural spray systems, coating formulations, textile finishing baths, and polyurethane reaction mixtures.
Unlike a simple dimethyl silicone oil, the modified material is designed to participate more effectively in complex formulations. It can be dispersed or dissolved in water and may also show partial or full compatibility with selected alcohols, esters, aromatic solvents, and other organic media, depending on its molecular structure and the composition of the surrounding system.
Its compatibility is not identical in every formulation. Factors such as polyether chain length, silicone-to-polyether ratio, temperature, pH, electrolyte concentration, solvent type, and the presence of other surfactants can influence final behavior. For this reason, product selection and application testing remain important parts of technical service.
2. Main Technical Advantages
2.1 Amphiphilic Compatibility
The most important advantage of polyether-modified silicone oil is its amphiphilic nature. The silicone segment is hydrophobic and possesses very low surface energy, while the polyether segment is more hydrophilic and polar. This combination allows the material to operate at the boundary between different phases.
In water-based systems, the polyether section supports dispersion and compatibility. On hydrophobic surfaces, the siloxane section promotes spreading and surface coverage. In mixed-solvent formulations, the molecule can help reduce the risk of rapid separation caused by poor interfacial compatibility. This makes it useful when a formulation contains water, polar solvents, active ingredients, resins, pigments, or other additives with different chemical characteristics.
Compared with traditional silicone oils, polyether-modified silicone oil generally offers better compatibility with water and polar components. Compared with many ordinary surfactants, it can provide more rapid spreading and stronger surface activity at relatively low use levels. These characteristics make it a useful bridge between silicone additives and conventional surfactant technologies.
2.2 Ultra-Low Surface Tension
Polyether-modified silicone oil can reduce surface tension to approximately 22 mN/m under suitable test conditions. The actual value depends on product grade, concentration, temperature, and test method, but the low-tension behavior is a key reason for its broad industrial use.
Lower surface tension allows droplets to contact difficult surfaces more efficiently. Instead of remaining as isolated beads, a liquid can spread over a larger area. In agricultural spraying, this may improve coverage of waxy or uneven plant surfaces. In coatings, it can support leveling and reduce surface defects. In textile finishing, it can promote more uniform treatment of fibers. In daily chemical products, it can improve the spreading feel of creams and lotions.
The material’s activity is not limited to spreading. It can also improve wetting and penetration by reducing the energy barrier between a liquid and a solid. This effect can support better contact with fibers, polymer films, pigments, coating substrates, and plant surfaces.
2.3 Stability and Weather Resistance
The siloxane structure contains strong silicon-oxygen bonds that contribute to thermal stability, aging resistance, and resistance to mechanical stress. As a result, polyether-modified silicone oil can maintain useful performance under changing environmental conditions, including hot and humid conditions as well as cold and dry conditions.
In practical production, the material may be exposed to shear during blending, pumping, spraying, coating, or foaming. A well-designed grade should maintain its intended interfacial function during processing rather than losing activity immediately under mechanical stress. The silicone structure also supports durable surface modification in applications where treated materials are exposed to heat, moisture, or outdoor conditions.
Weather resistance does not mean that every grade is suitable for every outdoor environment. Long-term performance depends on the complete formulation, ultraviolet exposure, pH, salts, temperature cycles, and substrate chemistry. Nevertheless, the combination of silicone stability and polyether compatibility gives the product an important advantage over many less durable organic surfactants.
2.4 Multifunctional Performance
Polyether-modified silicone oil can serve more than one purpose in a formulation. Depending on dosage and system design, it may function as a wetting agent, spreading agent, leveling additive, release modifier, foam stabilizer, surface conditioner, or formulation assistant.
This multifunctional behavior can reduce the number of separate additives required in a product. Fewer additives may simplify raw material management, reduce compatibility risks, shorten formulation development time, and improve process control. The most suitable role depends on the product grade and the target application.
| Performance characteristic | Contribution from the silicone segment | Contribution from the polyether segment | Resulting benefit |
|---|---|---|---|
| Surface activity | Low surface energy and rapid spreading | Interfacial compatibility | Efficient wetting of difficult surfaces |
| Water compatibility | Flexible molecular structure | Polarity and hydrophilicity | Improved dispersion in aqueous systems |
| Stability | Strong silicon-oxygen framework | Adjustable formulation interaction | Reliable performance in complex systems |
| Lubricity and softness | Smooth, flexible siloxane chain | Controlled deposition | Improved textile and surface feel |
| Foam control | Silicone interfacial activity | Compatibility with polar components | More controlled foam formation or reduction |
3. Molecular Structure and Performance Control
3.1 Role of the Silicone Backbone
The silicone backbone gives the material its characteristic low surface energy, flexibility, and spreading ability. Siloxane chains rotate easily and can move rapidly across an interface. This molecular mobility helps the additive reach the surface of a substrate or the boundary between two incompatible phases.
The backbone also supports thermal and chemical stability. Silicone materials are often selected for applications where ordinary organic additives may volatilize, decompose, or lose their surface function during processing. The exact stability of a product remains dependent on temperature, exposure time, surrounding chemicals, and molecular design, but the siloxane framework provides a strong foundation for durable performance.
3.2 Role of the Polyether Chain
Polyether chains introduce oxygen-containing ether groups that interact with water and other polar substances. Increasing the polyether contribution generally improves water compatibility, emulsification, and dispersibility. It can also change viscosity, cloud point, foaming tendency, and interaction with other surfactants.
Shorter polyether chains often preserve more of the silicone-like character. Such structures may provide strong spreading, low surface tension, and a greater tendency to interact with non-polar or low-energy surfaces. Longer polyether chains generally increase hydrophilicity and can make the material more suitable for water-based formulations.
The best balance depends on the intended use. A product for agricultural spray adjuvants may require excellent water compatibility and rapid spreading. A grade for release control or surface treatment may require stronger silicone character. A grade for polyurethane foam may need a carefully controlled balance between emulsification, cell stabilization, and foam behavior.
3.3 Silicone-to-Polyether Ratio
The ratio between silicone segments and polyether segments is a central design parameter. A higher silicone ratio typically supports stronger surface activity, lubrication, and spreading on hydrophobic substrates. A higher polyether ratio generally improves water compatibility and interaction with polar components.
Neither a high silicone ratio nor a high polyether ratio is universally better. Excessive silicone character may create compatibility challenges in some aqueous systems. Excessive polyether character may reduce the desired spreading effect or alter foam behavior. Product development therefore requires control of the ratio rather than maximizing a single property.
3.4 Block and Graft Architectures
Polyether-modified silicone oils may be designed with block structures, graft structures, or other molecular arrangements. Block structures place silicone and polyether regions in more defined sections of the molecule. Graft structures attach polyether chains along a silicone framework.
These architectures can influence viscosity, cloud point, wetting speed, emulsification, compatibility, and the distribution of the additive at an interface. A graft arrangement may support more uniform property distribution, while a block arrangement may provide a distinct balance between hydrophobic and hydrophilic behavior. The appropriate structure depends on the intended formulation and processing conditions.
3.5 Viscosity and Flow Behavior
Molecular structure affects viscosity and flow. Increased polyether content may raise viscosity and enhance interaction with polar components. Silicone-rich structures may maintain lower viscosity and smoother flow. These differences affect metering, pumping, blending, dilution, and final application.
Manufacturers and formulators should consider viscosity at the actual processing temperature rather than relying only on a single room-temperature value. Storage conditions, dilution procedures, shear rate, and the concentration of other ingredients may also affect the apparent flow behavior of the final formulation.
4. Advantages Compared with Conventional Alternatives
4.1 Compared with Traditional Silicone Oils
Traditional dimethyl silicone oils are known for low surface tension, lubrication, water repellency, and thermal stability. However, their limited compatibility with water and polar materials can restrict their use in modern water-based formulations. They may require emulsifiers, special dispersion methods, or additional processing steps.
Polyether modification improves the interaction between the silicone material and aqueous or polar phases. This can reduce the risk of floating oil, phase separation, uneven deposition, or unstable dilution. The modified material retains much of the silicone oil’s surface activity while offering greater formulation flexibility.
4.2 Compared with Ordinary Organic Surfactants
Many conventional organic surfactants offer good water solubility and emulsification but may not match the spreading speed, low surface energy, or durability of silicone-based materials. Some organic surfactants may also be more sensitive to temperature, electrolytes, pH, or long-term environmental exposure.
Polyether-modified silicone oil provides a different performance profile. The silicone segment promotes rapid spreading and surface modification, while the polyether segment supports compatibility. This combined mechanism can produce more efficient wetting at lower dosage in selected systems, although dosage must always be established through application testing.
4.3 Compared with Single-Function Additives
Single-function additives may require separate wetting agents, leveling agents, defoamers, lubricants, or release modifiers. Using multiple additives increases the possibility of interaction problems. One additive may reduce the effectiveness of another, create foam, destabilize an emulsion, or cause surface defects.
A multifunctional polyether-modified silicone oil can simplify the additive package when its performance matches the requirements of the system. It may provide wetting and leveling together, or emulsification and foam stabilization in polyurethane production. This does not eliminate the need for formulation design, but it can reduce complexity and improve development efficiency.
5. Agricultural Applications
5.1 Wetting and Spreading on Plant Surfaces
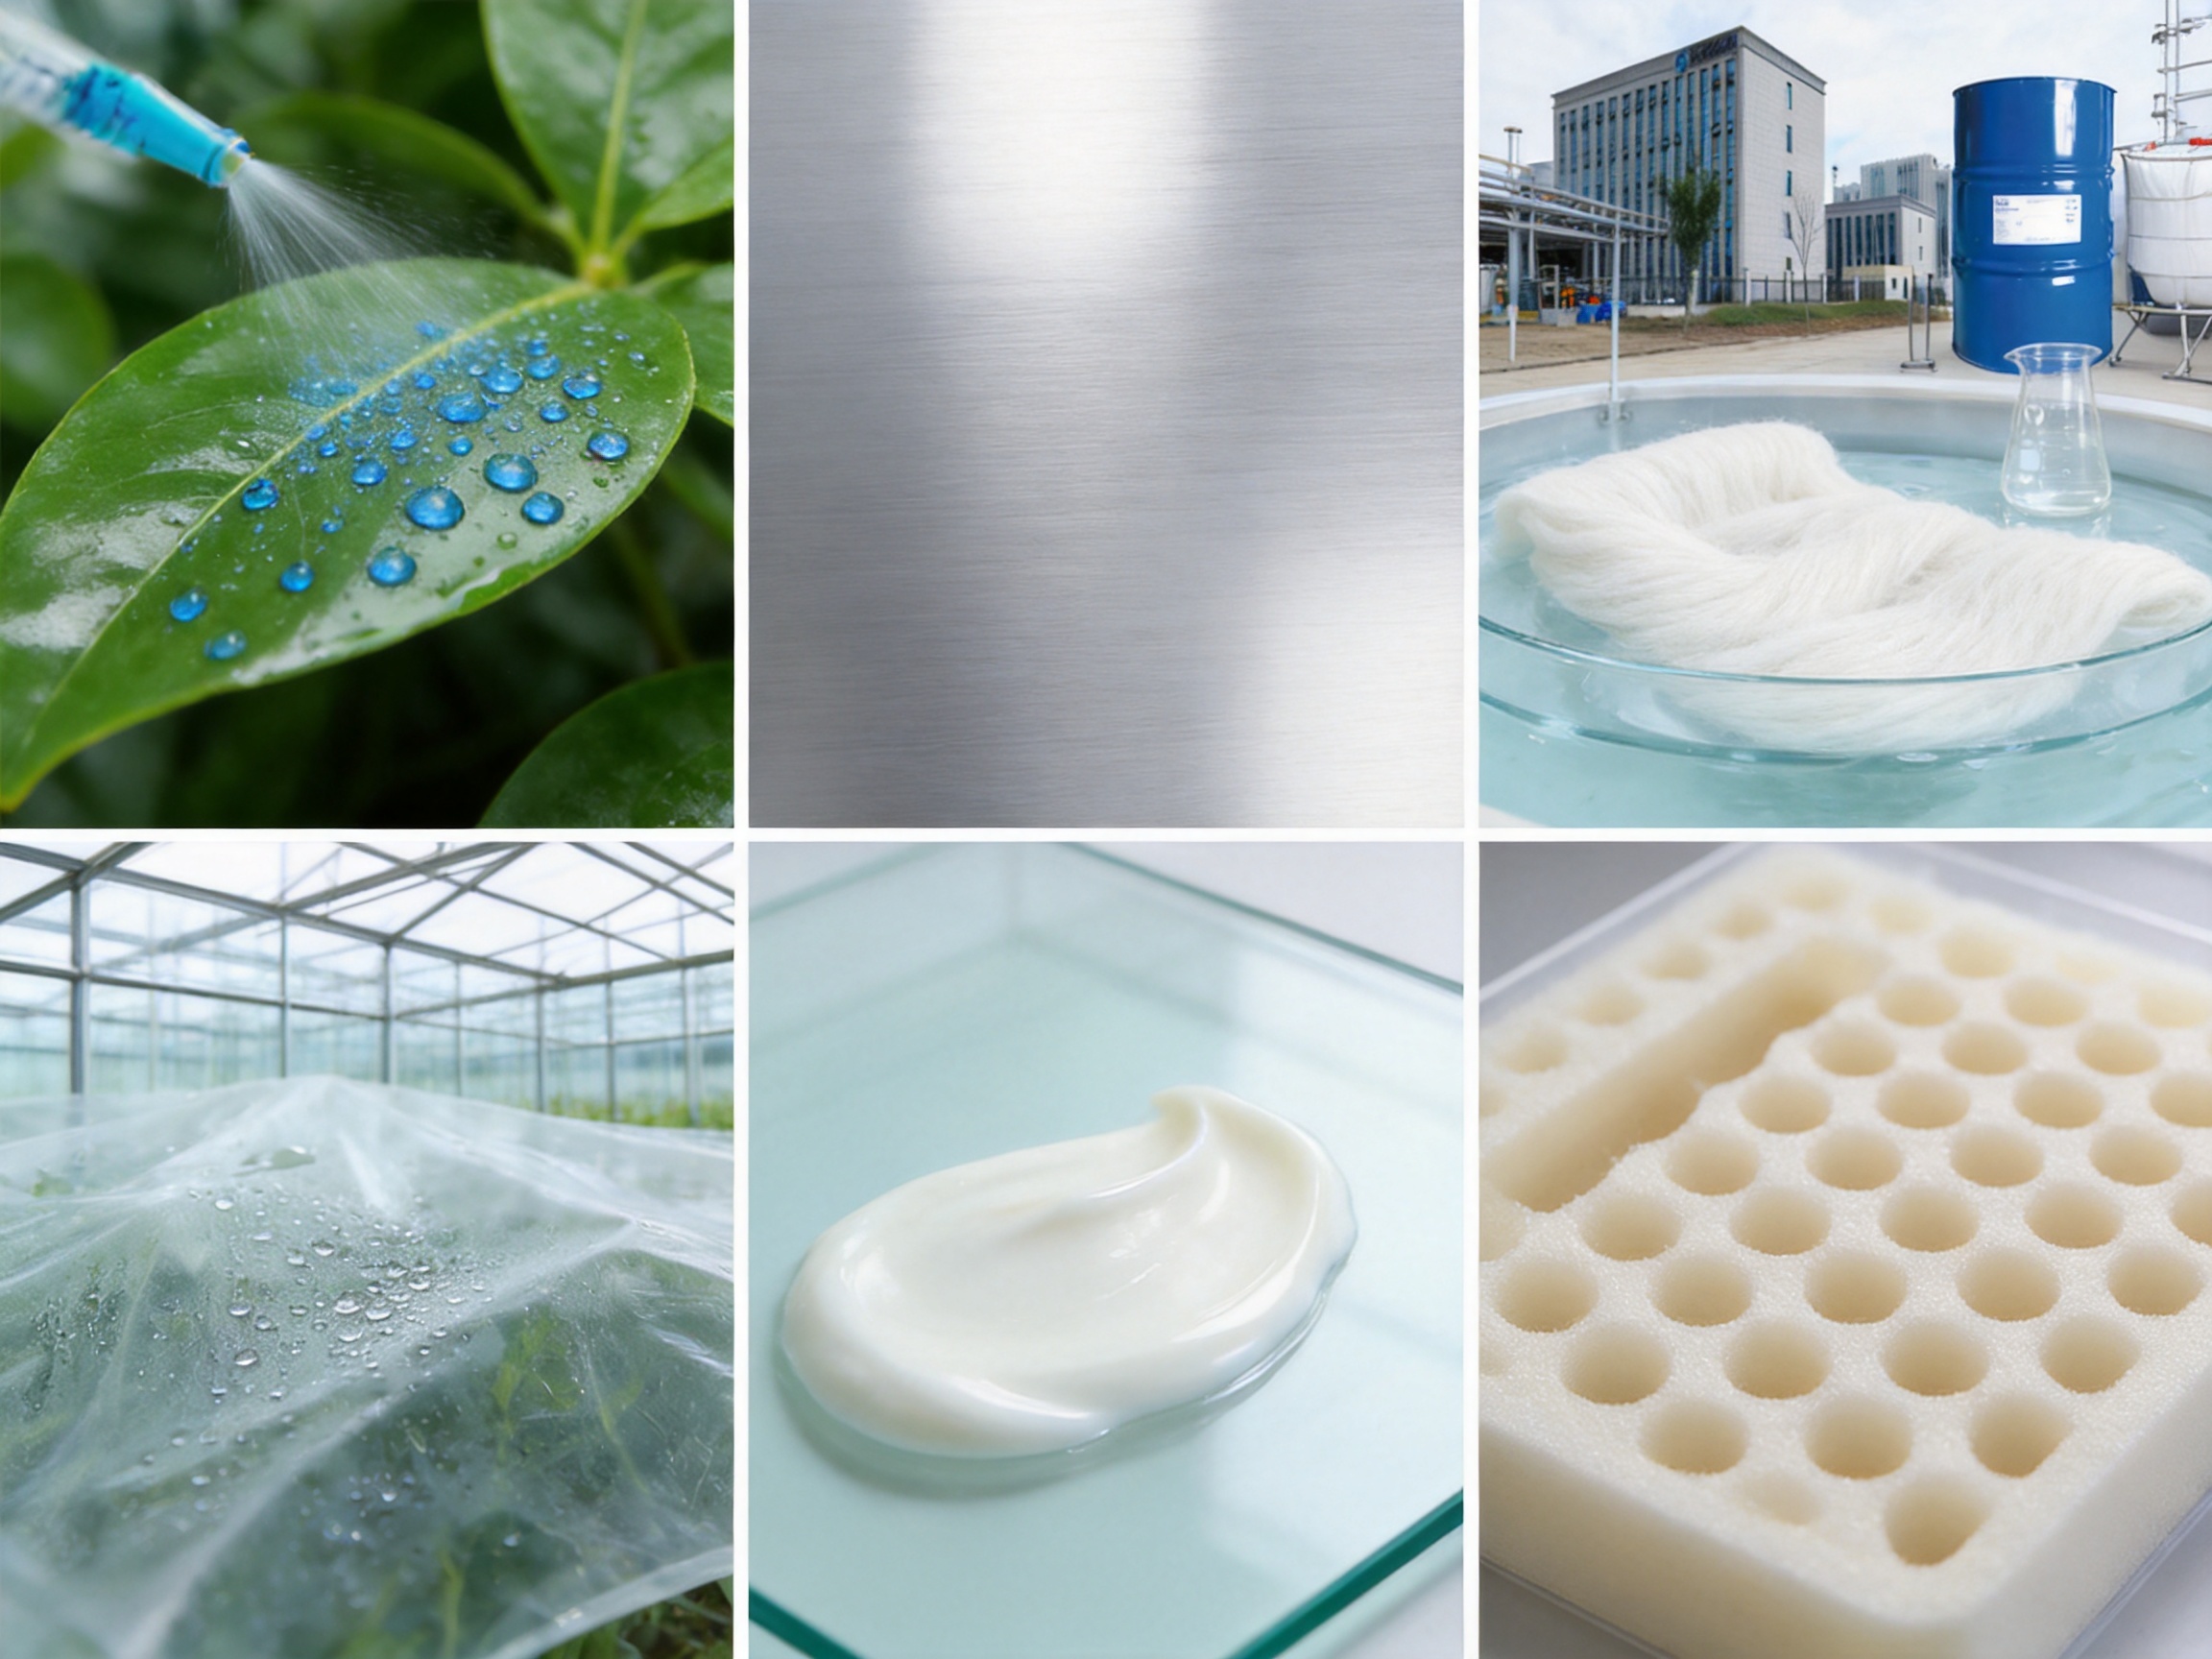
Agricultural formulations often need to cover plant leaves, stems, fruit surfaces, or other biological substrates that may be waxy, uneven, or naturally water-repellent. A water droplet with high surface tension may remain spherical and provide incomplete coverage. Polyether-modified silicone oil reduces the interfacial tension and enables the liquid to spread more efficiently.
Better spreading can support more uniform distribution of active ingredients and improve contact between the spray solution and the target surface. It may also reduce the tendency of droplets to remain concentrated in isolated spots. The practical result depends on spray equipment, weather, leaf structure, dosage, formulation composition, and the properties of the agricultural active ingredient.
5.2 Compatibility with Water-Based Agrochemical Systems
Many modern agrochemical formulations are water-based or are diluted with water before application. A suitable agricultural organosilicon additive must therefore disperse rapidly and remain stable during dilution. Polyether-modified silicone oil is designed to improve interaction with water while maintaining strong surface activity.
It may be used in systems containing herbicides, fungicides, insecticides, plant growth regulators, fertilizers, and other formulation components. Compatibility should be checked individually because salts, solvents, emulsifiers, active ingredients, and pH modifiers can change the final behavior of the product.
5.3 Agricultural Formulation Benefits
Potential benefits in agricultural formulations include improved wetting, more uniform spreading, reduced spray retention on equipment surfaces, improved contact with plant surfaces, and better dispersion of selected active ingredients. The additive may also help reduce the amount of water required for effective coverage in some application systems.
These benefits should not be interpreted as a guarantee of increased biological efficacy in every crop or formulation. Agricultural performance must be evaluated through laboratory testing, greenhouse trials, field testing, and compliance with applicable regulations. Correct use rates and tank-mix procedures are also essential for crop safety.
5.4 Agricultural Product Selection
Selection should consider water quality, hardness, electrolyte concentration, active ingredient chemistry, spray volume, crop type, leaf surface, temperature, humidity, and expected rainfastness. A grade with stronger water compatibility may be preferred for certain aqueous systems, while a grade with stronger spreading may be better for difficult hydrophobic surfaces.
Technical support is particularly valuable because the same additive may behave differently in concentrated formulations and in final spray dilution. Jar testing, accelerated storage testing, surface-tension measurement, contact-angle evaluation, and spray-coverage testing can help determine suitability.
6. Coatings and Inks
6.1 Leveling and Surface Appearance
In coating and ink formulations, surface tension differences can cause craters, pinholes, orange peel, poor leveling, uneven gloss, and inconsistent film appearance. Polyether-modified silicone oil can migrate toward the coating surface and reduce interfacial tension, helping the liquid level more smoothly before curing or drying.
The product information indicates that the additive can reduce coating surface tension from approximately 45 mN/m to 28 mN/m in a representative application. It is also associated with a significant reduction in orange peel defects and a decrease in spraying loss under suitable formulation conditions.
Actual results depend on resin type, pigment loading, solvent package, application method, film thickness, curing speed, substrate energy, and additive dosage. Excessive surface activity may create recoatability or adhesion problems in some systems, so optimization is necessary.
6.2 Compatibility with Water-Based Coatings
Water-based coatings require additives that can operate in a polar medium while still modifying the surface effectively. The polyether portion of the molecule supports compatibility with water and polar components, while the silicone portion reduces surface tension and improves leveling.
This balance can be useful in architectural coatings, industrial finishes, printing inks, wood coatings, plastic coatings, and other systems where low odor, water dilution, and smooth appearance are important. Compatibility with the resin and other additives should be confirmed through storage and application testing.
6.3 Foam Control and Surface Defects
Coating and ink production can introduce air through high-speed dispersion, pumping, filling, or spraying. Polyether-modified silicone oil may contribute to foam management depending on molecular design and dosage. It can also improve the smoothness and gloss of the cured film.
Foam control and leveling are related but not identical functions. An additive that is excellent for leveling may not be the best choice for aggressive defoaming. Product selection should therefore be based on the dominant process problem and tested under actual production conditions.
7. Textile and Dyeing Applications
7.1 Softening and Handle Improvement
Textile finishing agents are used to improve softness, smoothness, drape, hand feel, and surface comfort. Silicone-based materials are widely recognized for their ability to deposit a smooth, flexible layer on fibers. Polyether modification improves the material’s interaction with water-based finishing baths and can support more uniform distribution.
For cotton fabrics, the supplied performance information indicates that the product can reduce bending stiffness by approximately 40% under representative conditions. The final effect depends on fabric construction, fiber type, pretreatment, bath concentration, curing or drying conditions, and finishing equipment.
7.2 Moisture Absorption and Antistatic Properties
Some silicone softeners can make a fabric highly hydrophobic, which may reduce moisture management. The inclusion of polyether segments provides a more balanced surface character and can support moisture absorption and antistatic behavior. This is useful for garments, home textiles, technical textiles, and synthetic-fiber blends.
Textile manufacturers can adjust the finish according to the desired balance between softness, hydrophilicity, sewability, static control, and durability after washing. The product may be incorporated into finishing formulations together with compatible emulsifiers, wetting agents, crosslinkers, or other textile auxiliaries.
7.3 Processing Considerations
Important processing factors include bath stability, dilution order, pH, water hardness, temperature, padding pressure, drying speed, and fabric residence time. The additive should be introduced in a manner that avoids local overconcentration or rapid incompatibility with other bath components.
Laboratory trials should measure softness, absorbency, whiteness, shade change, yellowing, friction, antistatic performance, and durability after laundering. These tests help textile producers determine the most suitable dosage and finishing sequence.
8. Daily Chemical and Personal Care Applications
8.1 Skin Feel and Spreadability
In skincare products, spreadability is an important sensory characteristic. A cream or lotion that spreads easily can feel lighter and more comfortable during application. Polyether-modified silicone oil can reduce spreading resistance and help create a smooth, uniform film on the skin.
The supplied application information describes a reduction in spreading resistance of approximately 70% and film formation within about three seconds under representative conditions. It also indicates the potential for long-lasting moisturization and an increase in the SPF value of physical sunscreens when used in suitable formulations.
Such results depend strongly on the complete cosmetic formula, including oils, emulsifiers, waxes, polymers, pigments, ultraviolet filters, humectants, and preservatives. The product must be evaluated for skin compatibility, regulatory status, odor, color, stability, and sensory profile before commercial use.
8.2 Formulation Stability
Polyether-modified silicone oil can help improve the compatibility of silicone materials with aqueous and polar cosmetic components. It may be used in creams, lotions, sunscreens, conditioners, cleansing products, makeup, and other personal-care formulations where a soft, smooth, and non-greasy feel is desired.
Cosmetic formulators should conduct freeze-thaw testing, centrifuge testing, accelerated aging, microbial evaluation, viscosity monitoring, and packaging compatibility studies. The additive should be evaluated at the intended concentration and in the final package rather than only in a simplified laboratory blend.
9. Plastics, Greenhouse Films, and Polyurethane
9.1 Greenhouse Plastic Films
In greenhouse plastic film applications, surface properties influence condensation, light transmission, water behavior, and agricultural service life. A polyether-modified silicone additive can help form a nanoscale water-repellent or surface-modifying layer on a polymer film.
The supplied information indicates a potential increase in light transmittance of approximately 35%, anti-fog performance for up to 180 days under representative conditions, and an extension of film service life by approximately three years compared with selected traditional products. Actual performance depends on resin type, film extrusion conditions, additive migration, weather exposure, ultraviolet radiation, and the design of the complete film formulation.
Improved anti-fog behavior can help reduce water droplets that scatter light and obstruct plant illumination. Improved light transmission may support greenhouse productivity, although crop performance must be assessed separately through controlled trials.
9.2 Polyurethane Foam Stabilization
Polyurethane foam production requires controlled emulsification, bubble nucleation, cell growth, cell stabilization, and, in some cases, cell opening. Silicone-based surfactants are commonly used because they can control the interface between the polymer-forming mixture and the gas phase.
Polyether-modified silicone oil can promote emulsification of the reaction components and support the formation of fine, uniform cells. It may help manage bubble formation, stabilization, and interconnection throughout the foaming process. This is important for flexible foam, rigid foam, molded foam, insulation materials, cushioning products, and other polyurethane systems.
Foam performance is highly sensitive to isocyanate index, polyol composition, catalysts, water content, blowing agents, temperature, mixing energy, mold conditions, and surfactant dosage. Small changes in silicone surfactant structure can produce major changes in cell size, density, airflow, resilience, and dimensional stability.
9.3 Processing Control
A reliable foam stabilizer should be evaluated through cream time, rise time, tack-free time, free-rise density, cell size, airflow, compression set, tensile properties, and dimensional stability. The optimum dosage must be established for each polyurethane system rather than transferred directly from another formulation.
10. Manufacturing Process and Quality Strengths
10.1 Controlled Raw Material Selection
Stable polyether-modified silicone oil begins with consistent raw materials. Silicone intermediates, polyether components, catalysts, stabilizers, and processing aids must meet defined specifications. Variations in molecular weight, functional group content, moisture, acidity, or impurity level can influence reaction behavior and final product performance.
A professional manufacturer establishes incoming inspection procedures for critical materials. These procedures may include appearance evaluation, viscosity measurement, moisture testing, acid or alkali value determination, and other analytical checks appropriate to the raw material. Supplier qualification and batch traceability further support stable production.
10.2 Molecular Design and Reaction Control
The production of polyether-modified silicone oil requires controlled incorporation of polyether segments into the silicone structure. Reaction temperature, catalyst concentration, feed rate, mixing efficiency, reaction time, and atmosphere can all influence molecular architecture.
Precise process control helps maintain the target balance between silicone and polyether components. It also supports consistent viscosity, appearance, compatibility, surface tension, and storage stability. A modern production line should be capable of controlling these parameters across different product grades and batch sizes.
10.3 Advanced Production Equipment
The company supporting this product has established production facilities equipped with advanced manufacturing equipment and testing instruments. Such equipment enables controlled heating, mixing, feeding, reaction, cooling, filtration, and filling. Proper equipment design is especially important for silicone materials because localized overheating, incomplete mixing, or contamination can affect final performance.
Closed or well-controlled processing systems can help reduce contamination and improve worker and environmental protection. Accurate metering systems support reproducible ratios of silicone and polyether components. Efficient heat transfer helps maintain stable reaction conditions and reduces batch-to-batch variation.
10.4 Full-Process Quality Monitoring
Quality control should extend from raw material receipt to finished-product delivery. In-process monitoring may include reaction temperature, viscosity development, appearance, pH where relevant, solids content, and other process indicators. Finished-product testing may include purity, viscosity, surface tension, water compatibility, storage stability, and appearance.
A full-process quality system allows the manufacturer to identify deviations early rather than relying only on final inspection. Batch records, retained samples, traceability systems, and defined release procedures support consistent delivery for industrial customers.
10.5 Testing and Application Support
Analytical testing is important, but application testing is equally valuable. Customers need to know how the product behaves in their specific coating, pesticide, textile bath, polymer, cosmetic, or polyurethane system. A manufacturer with technical expertise can support screening tests, compatibility evaluations, dosage optimization, and troubleshooting.
Application-focused testing may include surface-tension measurement, contact-angle testing, emulsification stability, foam-height evaluation, leveling assessment, coating appearance, textile softness, spray coverage, and accelerated storage. These tests connect laboratory data with real production performance.
10.6 OEM and ODM Capabilities
Different customers may require different viscosity ranges, compatibility profiles, packaging formats, or performance balances. OEM and ODM services allow a manufacturer to adjust product specifications or develop a grade for a particular application.
Customization may involve modifying silicone-to-polyether balance, water compatibility, foam behavior, surface activity, viscosity, or packaging. A structured development process should include a clear technical brief, laboratory screening, pilot production, application validation, specification confirmation, and ongoing quality monitoring.
10.7 Supply Reliability
Industrial customers require more than a technically effective additive. They also need stable availability, consistent batch quality, responsive communication, suitable packaging, and reliable delivery. A company with integrated research, production, sales, and quality systems is better positioned to support long-term supply programs.
The manufacturer associated with this product has developed a broad product matrix covering silicone additives, wetting agents, modified silicone oils, dimethyl silicone oils, surfactants, defoamers, and related materials. This portfolio supports cross-product technical coordination and helps customers find compatible additive solutions within one supply network.
11. Recommended Formulation and Handling Practices
11.1 Compatibility Testing
Before commercial use, polyether-modified silicone oil should be tested with all major formulation components. A basic compatibility study may include visual observation, viscosity measurement, centrifuge testing, freeze-thaw cycles, heat aging, dilution stability, and surface-performance evaluation.
Testing should be performed at the expected use concentration and at several nearby concentrations. A formulation may appear stable at one dosage but separate or foam excessively at another. The order of addition should also be evaluated because premixing with water, solvent, resin, or surfactant can affect the final dispersion.
11.2 Dosage Optimization
More additive does not always produce better performance. Excessive dosage may cause surface defects, foam, poor recoatability, reduced adhesion, excessive slipperiness, or instability. The optimum level should be determined by comparing wetting, spreading, leveling, foam, storage, and final-use performance.
A practical screening program may begin with a low, medium, and high dosage. The results can then be used to identify the most efficient range. For agricultural formulations, spray coverage and plant safety should be included. For coatings, gloss, cratering, adhesion, and recoating should be measured. For textiles, softness, absorbency, and laundering durability should be assessed.
11.3 Storage
The product should be stored in a clean, sealed container in a cool and dry location. Direct sunlight, extreme temperatures, water contamination, and prolonged exposure to incompatible materials should be avoided. Storage recommendations may vary by grade and packaging, so the product technical data sheet and safety documentation should be followed.
Before use, the container should be inspected for sediment, separation, crystallization, unusual odor, or color change. If the product has been stored for an extended period, gentle homogenization may be considered when permitted by the product specification. Customers should not apply strong heat or aggressive mechanical treatment without technical guidance.
11.4 Safety and Regulatory Review
Industrial and agricultural users should review the applicable safety data sheet, labeling requirements, transportation rules, occupational exposure information, and regional regulations. Personal protective equipment and suitable ventilation should be used during handling and formulation.
For agricultural and cosmetic applications, regulatory requirements can be particularly specific. The user is responsible for confirming that the additive and the final formulation comply with the requirements of the target market and intended use.
12. Product Information
| Item | Information |
|---|---|
| Product name | Polyether-Modified Silicone Oil |
| Product model | LD-810 |
| CAS No. | 68937-55-3 |
| EINECS No. | 614-823-3 |
| Purity | 99.8% |
| Synonym | Polyether Silicone Surfactant |
| Primary functions | Wetting, spreading, leveling, emulsification, foam stabilization, surface modification, and release assistance |
| Main application sectors | Agriculture, textiles, coatings, inks, daily chemicals, plastics, greenhouse films, and polyurethane |
13. Why Choose an Experienced Silicone Material Supplier?
Polyether-modified silicone oil is not a simple commodity surfactant. Its performance depends on molecular architecture, formulation compatibility, processing history, and application conditions. An experienced supplier can provide more than a specification sheet by helping customers understand the relationship between product structure and final-use performance.
Technical experience is particularly important when a customer is replacing a conventional silicone oil, improving a water-based formulation, reducing coating defects, developing an agricultural adjuvant, or optimizing polyurethane cell structure. The supplier should be able to discuss product selection, dosage, dilution, storage, testing, and troubleshooting.
The company behind this product integrates research and development, production, sales, and technical support. Its product portfolio covers several categories of silicone-based materials and related additives. This integrated structure supports product customization, coordinated quality control, and long-term customer service.
The company also reports service to domestic agrochemical enterprises and exports to overseas markets including Europe and Southeast Asia. Stable performance, reliable quality, repeat purchasing, and support for OEM and ODM orders are important indicators for customers seeking a long-term supplier relationship.
For customers with complex requirements, the combination of production capability, testing facilities, experienced technical staff, and application knowledge can shorten the development cycle. It can also help reduce the risk associated with selecting an additive solely by price or by a single laboratory parameter.
14. Frequently Asked Questions
Q1: What is polyether-modified silicone oil?
Polyether-modified silicone oil is an amphiphilic silicone material containing siloxane segments and polyether segments. The silicone part provides low surface energy, spreading, flexibility, and thermal stability, while the polyether part improves water compatibility, polarity, dispersion, and interaction with polar materials.
Q2: What is the main advantage of this product over ordinary silicone oil?
The main advantage is improved compatibility with water-based and polar formulations while preserving strong silicone-based surface activity. It can reduce surface tension, improve wetting, and spread over difficult surfaces with less risk of separation than many conventional silicone oils.
Q3: Can polyether-modified silicone oil dissolve in water?
Many grades are designed to be completely miscible with water or to disperse readily in water, but behavior depends on the molecular structure and concentration. Water quality, temperature, electrolytes, pH, and other formulation ingredients can influence compatibility. A product-specific test should be conducted before large-scale use.
Q4: What surface tension can the product achieve?
The product information indicates that surface tension can be as low as approximately 22 mN/m under suitable conditions. The measured value depends on concentration, temperature, test method, and the composition of the surrounding system.
Q5: Is it suitable for agricultural formulations?
Yes. Its combination of water compatibility, low surface tension, rapid spreading, and wetting performance makes it suitable for many agricultural formulations. It may improve spray coverage on hydrophobic or uneven plant surfaces. Crop safety, active ingredient compatibility, dosage, and regulatory compliance must be evaluated before commercial application.
Q6: Can it be used with nonionic and anionic surfactants?
Polyether-modified silicone oil generally shows good compatibility with many nonionic and anionic surfactants. However, compatibility depends on the complete formulation. Jar testing, accelerated storage, dilution testing, and application evaluation are recommended.
Q7: Can it reduce orange peel in coatings?
It can support leveling by lowering surface tension and improving the flow of a coating film. The supplied information associates the product with a significant reduction in orange peel under representative conditions. Actual performance depends on resin, solvent, pigment, application method, film thickness, curing, and dosage.
Q8: Is it suitable for textile softening?
Yes. The silicone structure can improve softness and smoothness, while the polyether structure supports compatibility with water-based finishing baths and can help maintain moisture absorption and antistatic properties. Textile trials should evaluate softness, absorbency, shade, yellowing, and durability after washing.
Q9: Can it be used in polyurethane foam?
It can be used as a foam stabilizer or formulation additive in selected polyurethane systems. It may support emulsification, bubble formation, cell stabilization, and cell interconnection. Foam performance must be optimized against polyol type, catalysts, blowing agents, water content, processing temperature, and machine conditions.
Q10: What factors determine the correct grade?
Important factors include polyether chain length, silicone-to-polyether ratio, viscosity, water compatibility, surface activity, cloud point, foam behavior, application temperature, pH, electrolyte content, and the desired final performance. The supplier should review the formulation and recommend a grade based on application testing.
Q11: Can the product be customized?
Customization may be available through OEM and ODM services. Potential adjustment areas include viscosity, water compatibility, surface tension, spreading speed, emulsification, foam stabilization, packaging, and application-specific performance. A technical specification and trial program should be established before production.
Q12: How should the product be stored?
It should generally be stored in a sealed container in a cool, dry, and clean environment away from direct sunlight, extreme temperatures, and contamination. The specific storage period and handling requirements should be confirmed through the product technical data sheet and safety documentation.
15. Conclusion
Polyether-modified silicone oil combines the low surface energy and spreading ability of silicone with the water compatibility and polarity of polyether. This molecular design gives it a broad performance range that includes wetting, spreading, leveling, emulsification, surface modification, foam stabilization, softness improvement, and release assistance.
Its low surface tension, wide solvent compatibility, weather resistance, and multifunctional behavior provide meaningful advantages over conventional silicone oils, ordinary organic surfactants, and narrowly focused additives. These advantages support applications in agricultural formulations, coatings, inks, textile finishing, daily chemicals, greenhouse films, plastics, and polyurethane foam.
The value of the product depends not only on its chemical identity but also on production consistency and technical support. Controlled raw materials, precise molecular design, advanced production equipment, full-process quality monitoring, application testing, and customization capabilities are all important for reliable industrial use.
With product model LD-810, customers can evaluate a silicone-based surfactant designed for demanding formulation environments. By selecting the appropriate structure, dosage, and processing method, formulators can use polyether-modified silicone oil to improve surface performance while maintaining compatibility and stability in complex systems.
References
1. Product technical information for LD-810 Polyether-Modified Silicone Oil, including composition characteristics, application areas, and stated performance data.
2. General principles of organosilicon chemistry and siloxane-based surface modification.
3. Technical literature on silicone-polyether surfactants, interfacial tension, wetting, spreading, and emulsification.
4. Industrial formulation practices for agricultural adjuvants, coating additives, textile finishing agents, and polyurethane foam stabilizers.
5. General quality-control principles for specialty chemical manufacturing, including raw material inspection, process monitoring, finished-product testing, and batch traceability.
6. Application testing methods for surface tension, contact angle, coating leveling, textile softness, foam-cell structure, and formulation stability.
Product: Polyether-Modified Silicone Oil

Contact Information
Tel : +86-400-138-5268
Email : [email protected]
Phone : +86-15128434888 / +86-13511051998
Add : Xinqiao Environmental Protection Industrial Park, Wen'an County, Langfang City, Hebei Province, China
Contact Information
Copyright © Hebei Guituo New Material Co., Ltd. All Rights Reserved.
